
Optimizing part design, material selection and order arrangement is the most effective way to cut CNC machining costs without sacrificing required tolerance and function. Below are practical recommendations for your drawings and projects.
1. Simplify part geometry
Avoid deep narrow cavities, extremely thin walls, tiny sharp internal corners and complex undercuts whenever possible. These features require special tools, multiple setups or 5-axis operations, which greatly raise machining time. Use large radius internal fillets where you can.
2. Relax non-critical tolerances
Tight tolerances add inspection and machining time. Mark strict tolerance only on functional mating surfaces. Leave non-matching areas with standard general tolerance. We will flag over-specified tolerance during our DFM review.
3. Choose cost-effective materials reasonably
High-grade alloy, titanium and pre-hardened tool steel cost more in raw stock and machining. If performance allows, switch to common grades such as EN AW-6061 aluminium instead of 7075, or standard stainless steel to save material and cutting time.
4. Optimize part size & stock material
Select standard-size raw material blanks. Custom oversized stock leads to extra waste and longer cutting time. Group multiple small parts onto one workpiece (nesting) to reduce setup time for batch orders.
5. Combine orders and increase batch quantity
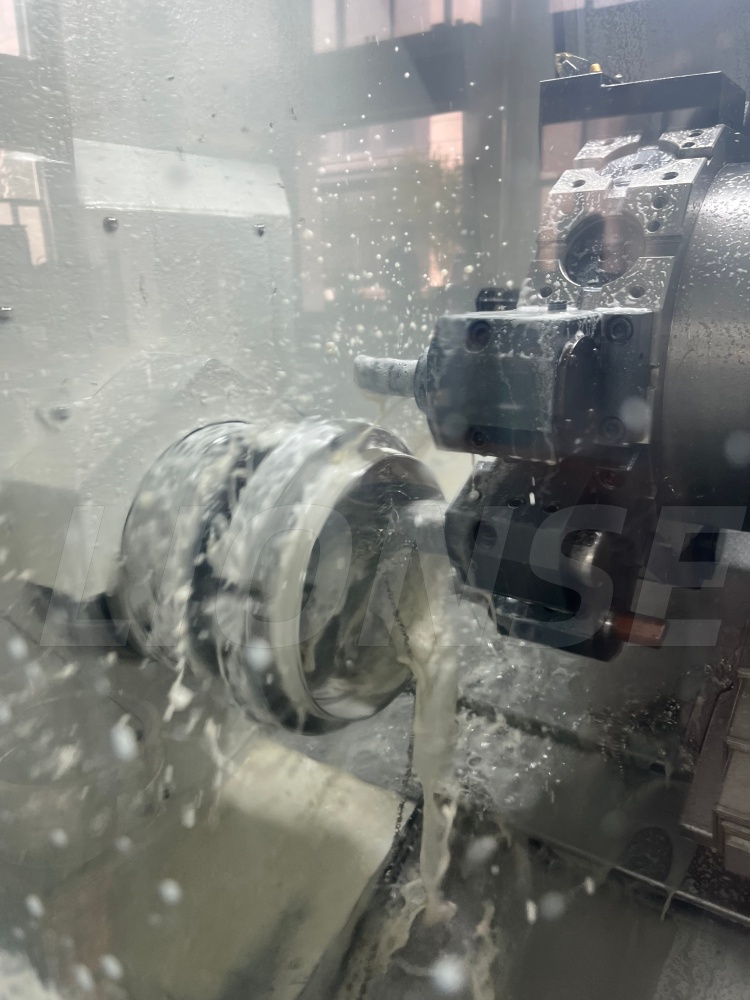
Setup cost is fixed for each production run. Consolidate separate small orders or raise batch volume to spread the fixture and programming cost over more pieces. Prototype + mass production combined orders also help reduce total unit price.
6. Reduce unnecessary surface treatments
Surface finishing like fine grinding, honing, mirror polishing or premium plating adds extra cost. Only specify surface finish and heat treatment for areas that need wear resistance, corrosion protection or sealing requirements.
7. Standardize threads, holes and features
Use standard metric thread sizes and standard drill diameters. Non-standard hole sizes and special threads require custom cutting tools, increasing tooling expense and lead time.
We balance cost, lead time and part performance. Our goal is to deliver functional precision components at the best possible price, not just to cut cost at the expense of quality.